Export-Grade Steel Castings for Global OEMs: Industry Expectations Explained

When an international OEM evaluates a new casting supplier, the conversation rarely starts with price. It starts with a much harder question: can this foundry consistently deliver parts that meet exacting metallurgical, dimensional, and documentation standards, shipment after shipment, regardless of order size or geography? For Austin Alloy Cast, a precision investment casting manufacturer based in Bharudi, near Rajkot in Gujarat, this question has shaped nearly every decision made since the company began operations in 2015.

What “Export-Grade” Actually Means

Export-grade is not a marketing phrase; it is a measurable set of expectations that global buyers apply before a single purchase order is signed. Material traceability, certified quality management systems, dimensional repeatability, and compliance with destination-country regulations all sit at the core of this definition. Austin Alloy Cast operates under ISO 9001:2015 for quality management, ISO 14001 for environmental management, and ISO 45001 for occupational health and safety. Beyond these baseline certifications, the company holds PED 2014/68/EU and AD 2000 Merkblatt W0 approvals, which are essential for supplying pressure equipment components into European markets, along with marine and offshore approvals from DNV GL, Lloyd’s Register, Bureau Veritas, and ABS. For offshore oil and gas applications, NORSOK M-650 approval for special materials adds another layer of qualification that many buyers specifically look for during vendor audits. The company has also aligned its practices with the EU’s Carbon Border Adjustment Mechanism, reflecting how export compliance now extends beyond metallurgy into carbon accounting and sustainable trade practice.

Precision as a Non-Negotiable Standard

Global OEMs, particularly those in oil and gas, heavy earth-moving equipment, food processing, and pulp and paper industries, work with tight engineering tolerances because even minor dimensional deviation can compromise assembly or performance in the field. Austin Alloy Cast’s lost-wax investment casting process is built to hold tolerances as tight as 0.1 millimetre depending on part geometry, with dimensional inspection carried out on coordinate measuring machines capable of 0.005 millimetre precision. This level of control matters because export shipments often travel thousands of kilometres before final assembly, and there is little room to rework a part once it reaches an overseas machining line or installation site. The company’s facility, spread across 75,000 square feet of constructed area within a 25,000 square metre plot, houses fully integrated departments for wax injection, shell coating, dewaxing, pouring, heat treatment, finishing, and testing, allowing every stage of production to be monitored under one roof rather than outsourced to third parties.

Material Range and Application Depth

International buyers rarely purchase “a casting”; they purchase a specific alloy engineered for a specific stress, temperature, or corrosion environment. Austin Alloy Cast’s material portfolio spans carbon steel, stainless steel, alloy steel, duplex and super duplex stainless grades, tool steel, and nickel- and cobalt-based alloys, covering applications from standard structural components to high-corrosion offshore environments. Casting weights range from a few grams up to 200 kilograms per piece, which allows the foundry to serve both small precision components and heavier industrial parts within the same production ecosystem. This breadth matters to OEMs who prefer consolidating multiple part families with a single qualified vendor rather than managing several regional suppliers.

Machining, Testing, and the Value of a Single Point of Contact

Modern OEMs increasingly expect suppliers to deliver finished, installation-ready components rather than raw castings that require further processing elsewhere. Austin Alloy Cast’s machining division operates CNC, VMC, HMC, and VTL centres, including equipment from established manufacturers such as Doosan, enabling the company to convert raw castings into fully machined parts complete with surface treatment, grinding, broaching, and lapping as required. Quality verification runs in parallel through an in-house laboratory offering non-destructive testing methods including radiography, ultrasonic testing, magnetic particle inspection, and dye penetrant testing, alongside destructive testing such as tensile, impact, and hardness evaluation. For buyers auditing potential suppliers, this in-house testing capability reduces dependency on third-party labs and shortens the verification cycle considerably.

Meeting Global Lead Time and Volume Expectations

Export buyers plan procurement cycles around realistic, disclosed lead times rather than optimistic promises. Austin Alloy Cast quotes typical lead times of 11 to 12 weeks for new product development and 12  weeks for repeat orders, figures that reflect the realities of pattern development, tooling validation, and multi-stage quality checks inherent to the lost-wax process. With an annual production capacity of approximately 1,800 metric tons at this single location, the facility is structured to handle both low-volume prototype runs and higher-volume repeat orders, a flexibility that many mid-sized OEMs specifically screen for during vendor selection.

Global Footprint and Documentation Readiness

Presence in a buyer’s own region often shortens the psychological distance between a foreign foundry and a domestic decision-maker. Austin Alloy Cast maintains a warehouse in North America and an office in Singapore, supplements this with a representative network across Europe and the Asia-Pacific region, and participates in international trade events including ValveWorld, ACHEMA, and CastForge. The company currently exports to markets including the United States, Germany, the United Kingdom, Italy, Canada, the Netherlands, Saudi Arabia, South Africa, Singapore, France, Spain, Romania, Sweden, Finland, and China. Every export shipment is supported with material test certificates, compliance documentation aligned to the importing country’s requirements, and coordinated packaging designed for long-distance freight, addressing one of the most common friction points international buyers report when working with new overseas foundries.

Why This Level of Rigour Matters to the Broader Industry

The global steel casting industry, valued in the tens of billions of dollars and continuing to grow at a mid-single-digit annual rate, has become considerably more scrutinised as OEMs consolidate their supply chains and demand fewer, more capable vendors. Buyers today expect a foundry to function less like a subcontractor and more like an extension of their own engineering team, offering material selection guidance, process consultation, and proactive quality reporting rather than simply fulfilling a purchase order. Austin Alloy Cast’s approach, combining certified quality systems, in-house testing, integrated machining, and disclosed production realities, reflects the standard that export-oriented OEM relationships increasingly demand, and offers a useful reference point for what “export-grade” should mean in practice rather than in promotional language alone.
How Heat Treatment Enhances Investment Casting Strength

Pull a steel casting straight out of the shell and you’re not looking at a finished component yet you’re looking at a part with a mechanical history it hasn’t resolved. Every casting cools unevenly. The outer surface, pressed against the ceramic mold, gives up its heat quickly. The core, insulated by the metal around it, lags behind. That mismatch leaves the part with patchy grain structure and locked in internal stress before it has done a single day of work. Heat treatment is the step that settles this account, and for OEMs specifying steel castings, it’s often the difference between a part that meets its mechanical spec and one that quietly falls short of it.

The Problem Hiding Inside an As Cast Part

Think of solidification as a race that different parts of the casting finish at different speeds. Thin sections and surfaces near the shell wall solidify fast, forming finer grains. Thick sections and interior mass cool slowly, forming coarser, less uniform grains. As the metal contracts on its way from liquid to solid, that uneven cooling also builds residual stress into the part stress that doesn’t show up on an inspection sheet but can surface later as distortion, cracking, or a fatigue failure nobody predicted from the tensile numbers alone.

This is exactly why a mill certificate showing the right chemistry isn’t enough on its own. Two castings poured from identical alloy can behave very differently in service if one went through a properly controlled thermal cycle afterward and the other didn’t.

How Controlled Heating and Cooling Fixes It

Heat treatment works by giving the casting a second chance at forming its internal structure this time under conditions the foundry controls rather than conditions dictated by geometry and mold behavior. The part is brought up to a specific temperature, held there long enough for the crystal structure to reorganize, then cooled at a rate chosen for the outcome that’s needed.

Depending on what the application demands, that cycle takes different forms:

A part that simply needs its grain structure refined and its as cast irregularities smoothed out is typically normalized heated above its transformation point and air cooled. This is often the first correction applied to carbon and low alloy steel castings before anything else happens to them.

When the priority shifts to easing machining and pulling out residual stress rather than maximizing strength, annealing is the better fit a slower furnace cool that softens the structure and makes downstream cutting and drilling operations more predictable.

Where a component needs real hardness alongside enough toughness to survive shock loading, the casting goes through quench and temper: a fast cool to lock in hardness, followed by a controlled reheat that trades away some of that hardness for ductility, so the part doesn’t behave like glass under impact.

Stainless steel castings carry their own complication welding and prolonged heat exposure can knock carbides out of solution and quietly erode the very corrosion resistance the grade was chosen for. Solution annealing puts those carbides back into solution and restores that protection.

And for castings with intricate geometry, where dimensional stability under later machining matters more than any property change, a stress relief cycle removes residual stress without disturbing the hardness the part already has.

What This Buys the Part, in Practical Terms

Done correctly, this thermal work shows up as measurable gains: tensile and yield strength climb as grain structure evens out; impact resistance improves, which matters most for parts facing shock loads or cold weather service; fatigue life extends because the internal stress that would otherwise start a crack has been driven out; machining goes more smoothly because the material responds to cutting tools more predictably; and for stainless grades, corrosion resistance is protected rather than gradually compromised by heat the part picked up during fabrication.

None of this happens by accident. Get the soak temperature, hold time, or cooling rate wrong, and a casting can come out of heat treatment weaker than it went in, which is precisely why the process needs to be controlled as tightly as the melt itself, not treated as an afterthought once the part is already shaped.

Where This Matters Most in Austin Alloy Cast’s Work

Our investment casting process is built around Fe and Ni based steel alloys, and the sectors we supply oil and gas, marine, heavy and earth moving equipment, and general engineering are exactly the sectors where a casting’s post heat treatment properties get checked, not assumed. Standards like NORSOK M 630 Ed. 6 for offshore components, or PED 2014/68/EU for pressure equipment, exist specifically because “the alloy was correct” isn’t proof enough that a part will perform; the thermal history has to be demonstrated too.

That’s why, on our floor, heat treatment and verification move together rather than as separate steps. Chemistry is confirmed on a spectrometer covering 36 elements across Fe and Ni based alloys, cross checked against certified reference material so composition drift that could throw off a heat treatment response gets caught before it becomes a problem. Once treatment is complete, dimensional integrity is confirmed by CMM inspection at ±0.005mm, and internal soundness is checked through 100% dye penetrant and magnetic particle testing, backed by radiography and ultrasonic testing wherever the application calls for it.

The Takeaway for Design Teams

A casting’s shape gets it through inspection on a drawing. Its heat treatment is what gets it through years of actual service. For anything headed into pressure retaining duty, marine exposure, or repeated cyclic loading, the thermal route chosen and how consistently a foundry can repeat it, batch after batch carries as much weight in service life as the alloy specified on the drawing.

If your design has specific mechanical targets in mind: a tensile threshold, impact toughness at low temperature, corrosion resistance that has to survive welding, that’s a conversation worth having during material selection, not after a prototype comes back under spec.

Working on a steel casting design with specific mechanical property requirements? Connect with Austin Alloy Cast’s technical team to discuss material and heat treatment selection for your application.

Understanding Nickel-Based Alloys in Investment Casting Applications

When a component has to survive inside, a chemical reactor, or a subsea pipeline, “strong enough” is not the standard; it has to hold its shape, its strength, and its surface integrity while everything around it tries to corrode, oxidize, or creep it out of tolerance. This is the world nickel-based alloys were built for, and it’s also the world where investment casting earns its keep. At Austin Alloy Cast, we work with these alloys regularly, and this post walks through what makes them behave the way they do, which grades are actually used in practice, and why the investment casting process suits them so well.

Why Nickel Is the Base Metal of Choice for Extreme Environments

Nickel-based alloys are built around a nickel matrix, typically over 50% nickel by weight, combined with elements like chromium, molybdenum, cobalt, iron, aluminum, titanium, and niobium. Each addition does specific work: chromium builds a protective oxide layer that resists oxidation and corrosion, molybdenum and tungsten add solid-solution strength and pitting resistance.

Most nickel-based alloys solidify into an austenitic (face-centered cubic) structure, which is inherently tough and ductile even at low temperatures, a real advantage over the alternatives in many industrial settings. This structure, combined with the alloying strategy above, is what lets nickel alloys operate reliably in the 650°C to 1000°C range, and in some grades, resist degradation even closer to their melting point.

Because of this combination of properties, nickel-based alloys are generally grouped by the job they’re optimized for:

  • Heat-resistant grades — built to resist oxidation, creep, and thermal fatigue at sustained high temperature
  • Corrosion-resistant grades — built to survive acids, chlorides, and marine or chemical process environments
  • Precipitation-hardened superalloys — built for maximum mechanical strength at elevated temperature
  • Wear-resistant and precision grades — used where dimensional stability or surface durability matters more than raw strength
The Grades That Actually Show Up on Foundry Floors

A handful of nickel alloy families account for the overwhelming majority of investment-cast nickel components in industry:

Inconel 625 is a nickel-chromium-molybdenum alloy (minimum ~58% nickel) that relies on solid-solution strengthening rather than heat treatment. It resists oxidation up to roughly 980°C and stands out for near-complete resistance to chloride-induced stress corrosion cracking, along with strong resistance to nitric, phosphoric, sulfuric, and hydrochloric acid environments. In the annealed condition, it typically delivers tensile strength in the 830–930 MPa range with elongation as high as 45–60%, which is exceptional ductility for an alloy this corrosion-resistant. This combination is why 625 dominates in marine hardware, seawater valves, submarine and naval propulsion parts, and chemical processing components.

Inconel 718 is the workhorse of the aerospace superalloy world; it’s reported to account for a very large share of global superalloy tonnage, largely because of its balance of cost, weldability, and high-temperature strength. Unlike 625, Inconel 718 is precipitation-hardened: niobium and titanium form γ’ and γ” strengthening phases during aging heat treatment, pushing aged tensile strength up to roughly 1,240–1,550 MPa and yield strength above 1,000 MPa nearly double that of annealed 625. Its practical service ceiling is lower, however, generally cited around 649–704°C, because the γ” phase overages and creep resistance drops sharply above that range. It’s the standard choice for jet engine components, gas turbine hardware, and other rotating parts where fatigue life and high-stress performance matter more than corrosion margin.

Hastelloy alloys (C-276, C-22, C-2000, and related grades) are nickel-molybdenum-chromium alloys purpose-built for aggressive chemical environments hot chlorides, sulfuric and hydrochloric acid service, and other conditions that would pit or crack lesser alloys. These are common in chemical processing and pollution-control equipment where corrosion resistance is the primary design driver.

Monel 400 and related nickel-copper alloys offer strong resistance to seawater and reducing acids and remain a standard choice in marine hardware and certain chemical processing applications where copper-nickel chemistry gives an edge over straight nickel-chromium systems.

Why Investment Casting Is the Right Process for These Alloys

Nickel superalloys are notoriously difficult to machine the same high-temperature strength and work-hardening behavior that make them valuable and also make them slow and tool-intensive to cut from bar stock. Investment (lost-wax) casting sidesteps much of that problem by producing a near-net-shape part directly from molten metal, which is precisely why it’s the dominant production route for complex nickel alloy components rather than an alternative to machining.

A few reasons this pairing works so well in practice:

  • Complex geometry without complex machining. Turbine blades, impellers, valve bodies, and manifold components often have internal passages, thin walls, or curved surfaces that would be extremely costly or impossible to machine from solid stock. Investment casting produces these shapes directly.
  • Reduced or eliminated secondary machining. Fine-grain investment casting, particularly with silica-sol shell processes, can reach tight dimensional and geometric tolerances straight out of the mold, cutting down the amount of hard-alloy machining required afterward.
  • Metallurgical consistency. Because the process controls solidification rate and mold environment closely, foundries can manage grain structure and minimize segregation, an important consideration for cast nickel superalloys, where issues like niobium segregation and Laves phase formation have historically been a challenge that heat treatment and process control are used to address.
What This Means for Component Selection

Choosing a nickel-based alloy for a cast component really comes down to three questions: What’s the operating temperature? What’s the corrosive environment? And how much mechanical load and fatigue cycling will the part see? A part destined for a jet engine hot section leans toward Inconel 718 or similar precipitation-hardened superalloys. A part destined for seawater or acid service leans toward Inconel 625, Hastelloy, or Monel. Getting this match right and casting to the correct AMS or equivalent specification rather than a generic “nickel alloy” is what determines whether a component lasts its intended service life or fails early.

At Austin Alloy Cast, this is the kind of alloy selection and process discipline we apply on every nickel-based investment casting project matching the right grade, the right melting practice, and the right quality control to the environment the part will actually operate in.

Certification vs Reality: How Austin Ensures Compliance on the Shop Floor

A certificate is a snapshot. It tells you a system was audited and found compliant on a given day. What it doesn’t show you is whether that same discipline holds up on the shop floor, batch after batch, when production pressure is high and deadlines are tight. For OEM buyers, that gap between paper and practice is exactly where casting quality either holds or breaks down.

At Austin Alloy Cast, our certifications are ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, PED 2014/68/EU, UKCA, IBR 1950, NORSOK M-630 Ed. 6, and marine approvals from DNV, ABS, Lloyd’s Register, BV, and RINA aren’t the end goal. They’re the audited proof of a shop floor system we run every day, regardless of whether an auditor is on site. Here’s what that actually looks like in practice.

Where Compliance Starts: Before the First Pour

ISO 9001:2015 requires contract review before production begins, and that’s not a paperwork formality at Austin every order starts with a documented review of feasibility, tolerances, and material requirements. That means the shop floor isn’t interpreting a customer’s drawing on the fly; the process parameters for wax injection, shell building, pouring, and heat treatment are defined and agreed before metal is melted.

This matters because most casting defects don’t originate at the pour they originate from an assumption made two steps earlier. A documented contract review closes that gap before it becomes a shop floor problem.

Chemistry and Metallurgy: Verified, Not Assumed

Certification standards for pressure equipment and marine applications, like NORSOK M-630 and PED 2014/68/EU, place heavy weight on material traceability and chemical accuracy. On our shop floor, this is backed by a spectrometer covering Fe and Ni based alloys across 35 elements, including nitrogen, and validated against CRM (certified reference material) samples for different steel families.

That’s the reality check behind the certificate: chemistry isn’t confirmed against a general tolerance band, it’s checked element by element, with reference standards that catch drift before it reaches a customer.

NDT: The Part of Certification You Can’t Fake

This is where “certification vs reality” gets tested hardest, because non-destructive testing is where hidden defects either get caught or get shipped. Austin runs:

  • 100% Dye Penetrant Testing for surface crack detection, per EN 1371-1 and ASME Section V Article 6 & 24
  • 100% magnetic particle testing for ferromagnetic components, under EN 1369 and ASME Section V Article 7 & 25.
  • Radiographic (X-ray) testing with Ir-192 and Co-60 sources, operated in separate in-house facilities in accordance with EN 12681 and ASME Section V Article 2 & 22.
  • Ultrasonic testing capability for additional volumetric inspection where specified.

The word that matters here is “100%” not sampled, not spot checked. Every applicable casting goes through dye penetrant and magnetic particle inspection, not a statistical subset. That’s the difference between a lab technically capable of meeting a standard and a shop floor that actually applies it to every part, every day.

Dimensional Accuracy: Where Tolerance Meets the CMM

A certificate can confirm a quality system exists; it can’t confirm a part fits. That verification happens on the shop floor through CMM (coordinate measuring machine) inspection at ±0.005mm precision, checking castings and machined components against CAD models before they ship. Our machining division runs CNC & VMC equipment from Jyoti, chosen specifically to hold that level of accuracy consistently across production runs, not just on a qualification sample.

Weld Repairs: Controlled, Not Concealed

Complex castings often need weld repair, and this is a point where “certified” foundries can quietly differ in practice. Austin’s WPS (Welding Procedure Specification) approvals mean any repair is carried out within qualified methods and limits, and welded zones are folded back into the same NDT plan as the rest of the casting. Nothing gets touched up and shipped without being re inspected under the same standards the original casting passed.

Marine Grade Standards as a Shop Floor Stress Test

Marine classification approvals are a useful proof point precisely because they’re hard to earn on paper alone. Austin holds approvals from DNV, ABS, Lloyd’s Register, and BV, and is RINA marine approved notably, the only pure play investment casting company in India with RINA accreditation, and only the sixth foundry group in the country to hold it at all. Earning that approval means demonstrating, under audit, that materials, process control, and inspection routines hold up to classification society scrutiny, not just general engineering tolerances. That’s a shop floor being tested against one of the more demanding real world benchmarks in the industry, not just a document being filed.

Environmental and Safety Systems, Running in the Background

ISO 14001:2015 and ISO 45001:2018 rarely get discussed in terms of casting quality, but they shape shop floor stability. Our operations partially run on 1.5 MW of solar power as part of environmental controls under ISO 14001, and workplace risk is systematically assessed under ISO 45001 both of which support a more stable, experienced workforce rather than one disrupted by preventable safety incidents or environmental non compliance.

What This Means for OEM Buyers

Certifications tell you a system was designed to be audited. What determines whether that system protects your program is whether the same rigor holds on an ordinary production day, not just an audit day. At Austin Alloy Cast, that’s the standard we hold ourselves to 100% NDT coverage where applicable, chemistry checked against certified references, dimensional verification at micron level precision, and repair work brought back into the same inspection loop as the original casting.

If you’re qualifying a casting supplier for a program where compliance isn’t optional, it’s worth asking not just which certificates a foundry holds, but how those standards translate into daily shop floor practice.

Steel Castings for the Automotive Sector: Meeting Strength, Safety & Scale Requirements

Automotive components live a demanding life. They absorb road shock, cycle through heat and cold, carry structural loads for years without failure, and in almost every case have to do it while meeting strict safety certifications and tight cost targets. For OEMs and Tier 1 suppliers sourcing cast components, steel casting sits at the intersection of three requirements that don’t always play well together: strength, safety, and scale.

At Austin Alloy Cast, we supply investment cast steel components into engineering and heavy duty applications where failure isn’t an option and volume isn’t negotiable. Here’s what automotive sourcing and design teams should understand about steel castings before locking in supplier decisions.

Why Steel Castings Still Matter in Automotive Manufacturing

Despite the industry’s ongoing shift toward lightweighting alternatives, steel castings remain essential wherever a component needs high strength to cost ratio, wear resistance, or the ability to survive repeated stress cycles. Steering knuckles, differential housings, suspension components, brake system parts, and various drivetrain elements are frequently cast in steel precisely because the material delivers predictable mechanical performance under real world abuse potholes, temperature extremes, and years of vibration.

Investment casting, in particular, allows automotive parts to be produced near net shape with complex geometries that would otherwise require extensive machining or multi part assemblies. That translates into fewer joints, fewer failure points, and often a lighter, more efficient part than a fabricated equivalent.

Strength: Designing for Real World Loads, Not Just Spec Sheets

Automotive components rarely fail under a single overload event; they fail from fatigue, accumulated over thousands of load cycles. This makes fatigue strength, not just tensile strength, one of the most important properties to specify correctly.

A few factors that influence real world strength performance:

  • Grain structure and porosity control. Even minor internal porosity can become a crack initiation point under cyclic loading. Casting process control matters as much as alloy selection.
  • Alloy selection matched to duty cycle. A part that sees constant vibration and shock loading, like a suspension component, needs different toughness characteristics than a static bracket.
  • Heat treatment consistency. Mechanical properties promised on a data sheet are only realized if heat treatment is controlled and repeatable across every batch, not just the first sample lot.

OEMs should push suppliers for process documentation, not just certified test results on isolated samples, batch to batch consistency is what actually protects a vehicle program from field issues.

Safety: Where Casting Quality Becomes Non-Negotiable

Automotive castings frequently go into safety critical systems steering, braking, suspension where a hidden defect can have consequences far beyond a warranty claim. This is where casting quality assurance stops being a formality and becomes core to the sourcing decision.

Key quality checkpoints that matter for automotive grade steel castings include:

  • Non-destructive testing such as radiography, dye penetrant, or magnetic particle inspection to catch internal or surface defects before parts ship.
  • Dimensional verification against CAD models, especially for parts that mate with other precision components.
  • Material traceability, so every casting can be traced back to its raw material heat and process batch if an issue ever surfaces in the field.
  • Certification to recognized standards, giving OEMs documented assurance that the casting process itself is controlled and auditable.

Automotive sourcing teams should treat a supplier’s quality system, not just their price quote, as a primary qualifying factor, particularly for any part with safety or regulatory implications.

Scale: Producing Consistently, Not Just Once

A prototype casting proving a design works is only half the challenge. Automotive programs need suppliers who can reproduce that same quality across production volumes that may run into the tens of thousands of units annually, without drift in dimensional accuracy or mechanical properties.

Scaling steel casting production reliably depends on:

  • Tooling design built for repeatability, not just first article approval.
  • Process capability, meaning a facility that can hold tight tolerances consistently across long production runs, not just under ideal single piece conditions.
  • Capacity planning, since automotive programs often need volume flexibility as vehicle demand shifts.
  • Value added machining and finishing integrated into the supply chain, reducing the number of external touchpoints between casting and finished parts.

This is also where facility scale genuinely matters. A foundry that can handle heavier per piece weights and larger production volumes at a single location reduces the coordination risk that comes from splitting production across multiple smaller suppliers.

What This Means for Design and Sourcing Teams

Before finalizing a cast steel component for an automotive program, it’s worth working through a short set of questions with your casting partner:

  • What is the actual fatigue and load profile the part will see in service, not just its static strength rating?
  • What non-destructive testing and traceability does the supplier apply as standard, versus what’s optional?
  • Can the supplier demonstrate consistency across production volume batches, not just prototype samples?
  • Are machining and secondary processes handled in house or through additional vendors, and how does that affect lead time and quality control?
  • Does the casting facility have proven capacity to scale with the program’s volume over its lifecycle?

Getting these answers early during design and supplier qualification prevents costly surprises once a part is locked into a vehicle program and production is running at full volume.

Partnering for the Long Run

Automotive steel castings sit under real pressure: they need to perform reliably for years, meet exacting safety expectations, and be producible at volume without variation. That combination rewards suppliers who treat process control, testing, and scalability as fundamentals rather than added extras.

At Austin Alloy Cast, we work with automotive and general engineering clients on investment cast steel components engineered for exactly this kind of demanding service from initial prototype through full production scale. If your program is evaluating cast component suppliers, it’s worth a technical discussion before designs are finalized.

Carbon Steel vs Alloy Steel Castings: What OEMs Should Know Before Finalizing Designs

For OEMs designing components that will spend years under load, heat, pressure, or corrosive exposure, the choice between carbon steel and alloy steel castings is rarely just a spec sheet decision. It shapes tooling costs, lead times, machining behavior, and most importantly how the part performs once it leaves the drawing board and enters the field. Getting this call right early saves rework, redesigns, and expensive field failures later.

At Austin Alloy Cast, we work with design and procurement teams across valve and pump, oil and gas, mining, marine, and heavy equipment industries who are weighing exactly this trade off. Here’s a practical breakdown of what actually separates the two, and how to think through the decision before a design gets locked in.

The Core Difference

Carbon steel castings derive their properties primarily from carbon content, with minimal additional alloying elements. They’re straightforward, cost effective, and well understood, a dependable choice when the application doesn’t demand exceptional resistance to heat, corrosion, or wear.

Alloy steel castings, on the other hand, are engineered with deliberate additions, chromium, nickel, molybdenum, manganese, vanadium, and others to achieve specific mechanical or environmental performance. These additions change how the metal behaves under stress, temperature swings, and chemical exposure, often at a higher material and processing cost.

Neither is inherently “better.” The right choice depends entirely on what the part needs to survive.

Where Carbon Steel Makes Sense

Carbon steel castings are a strong fit when:

  • The operating environment is relatively gentle, no aggressive chemicals, minimal thermal cycling, moderate loads.
  • Cost control and shorter lead times matter more than marginal performance gains.
  • The part will be coated, painted, or otherwise protected from corrosion externally.
  • Machinability and weldability are priorities, since carbon steel generally machines and welds more predictably than higher alloy grades.

Structural brackets, housings, general engineering components, and parts operating in controlled indoor environments often fall into this category. If an OEM is producing high volumes of a component that doesn’t face harsh service conditions, carbon steel usually delivers the best balance of performance and cost.

Where Alloy Steel Earns Its Premium

Alloy steel castings justify their added cost when the part faces one or more of the following:

  • High temperature service — alloys with chromium and molybdenum resist softening and scaling at elevated temperatures far better than plain carbon steel.
  • Corrosive or wet environments — oil and gas wellheads, marine hardware, and chemical processing equipment routinely need the corrosion resistance that alloying provides.
  • High wear or abrasive contact — mining, earth moving, and material handling components benefit from alloys engineered for hardness and toughness together.
  • Critical structural loads — where fatigue resistance and toughness at both high and low temperatures cannot be compromised.

For valve and pump bodies handling aggressive media, or earth moving components subject to constant abrasive wear, alloy steel isn’t a luxury; it’s what keeps the part from failing well before its expected service life.

Design Considerations OEMs Often Overlook

Section thickness and casting behavior. Alloy steels can behave differently during solidification than carbon steel, affecting shrinkage patterns and the likelihood of porosity in thicker sections. Designs should account for this early rather than adjusting after tooling is cut.

Machining allowances. Higher alloy grades often require different cutting parameters and tooling. If your part has tight tolerances or complex machined features, factor this into both cost estimates and lead time expectations.

Weldability for repairs or assembly. If the component will need field welding or repair down the line, some alloy grades require preheating and controlled cooling to avoid cracking, a maintenance consideration that’s easy to miss at the design stage.

Heat treatment requirements. Many alloy steel castings need post cast heat treatment to achieve their intended mechanical properties. This adds a process step and should be built into project timelines from the start, not discovered mid production.

Total cost of ownership, not just unit price. A carbon steel part that fails or corrodes within two years can cost far more in downtime, replacement, and warranty claims than a slightly pricier alloy steel casting that lasts the full service life. OEMs designing for harsh or critical applications should weigh lifecycle cost, not just quoted price per piece.

A Practical Way to Decide

Before finalizing a casting material, it helps to walk through a few direct questions:

  • What is the actual operating environment, temperature range, chemical exposure, load type?
  • What is the expected service life, and what does failure cost in downtime or safety terms?
  • Does the part require specific mechanical properties like impact toughness at low temperatures, or hardness for abrasion resistance?
  • What are the machining, welding, and heat treatment implications for each material option?
  • How do total lifecycle costs compare, not just initial casting price?

Answering these questions with real application data rather than defaulting to habit or the cheapest quoted option is what separates designs that perform reliably from those that need costly revisions after field deployment.

Getting It Right From the Start

Choosing between carbon steel and alloy steel castings isn’t just a materials question, it’s a design decision with downstream effects on manufacturability, cost, and long term reliability. The best outcomes happen when material selection is part of the conversation from the earliest design stages, not an afterthought once tooling is already underway.

At Austin Alloy Cast, we work alongside OEM engineering teams through the investment casting process from material selection and prototype development to full production to make sure the castings specified actually match the demands of the application. 

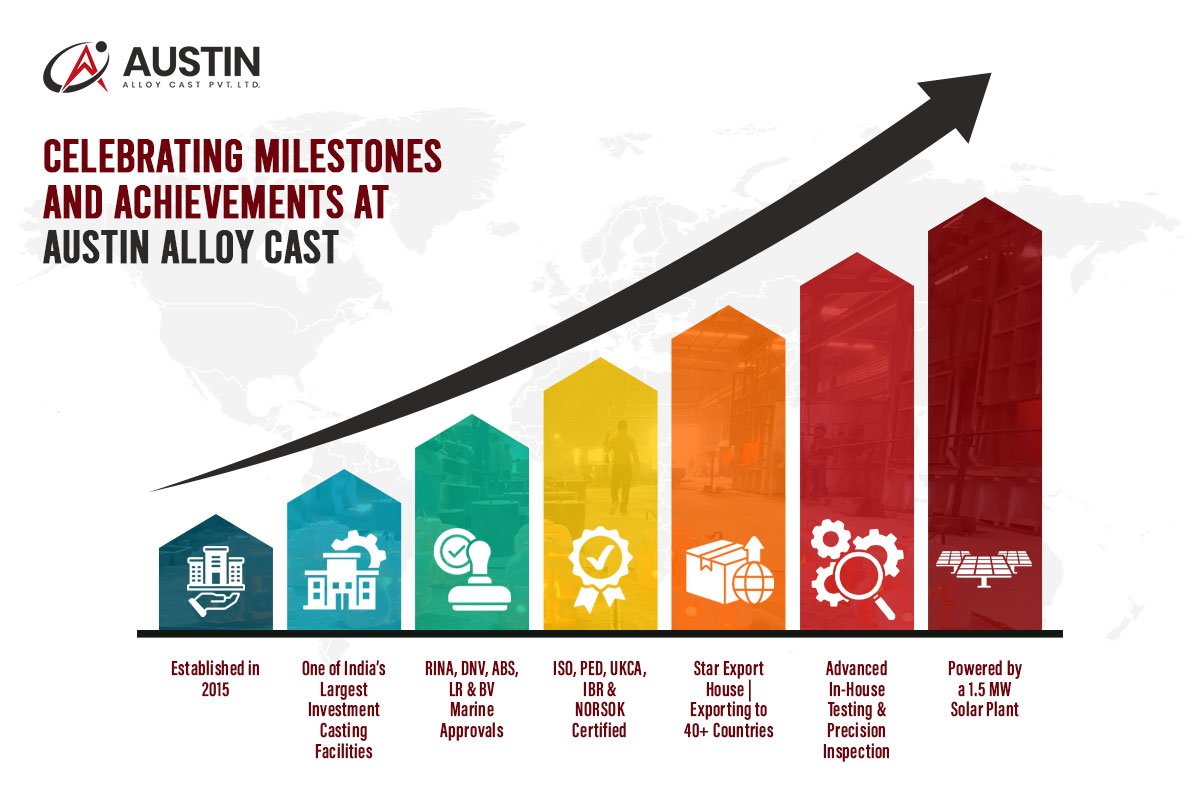
Celebrating Milestones and Achievements at Austin Alloy Cast

Every certification, facility expansion, and export approval a company earns is a marker of a decision made years earlier, usually the harder one, not the easier one. At Austin Alloy Cast, our milestones aren’t trophies on a shelf; they’re proof points of a strategy we’ve followed since our founding: build one large, fully integrated facility, invest in real testing infrastructure, and earn recognition the slow way, through audits and performance rather than claims. Here’s a look at where that strategy has taken us.

Building One of India’s Largest Single Location Investment Casting Facilities

Austin Alloy Cast was established in 2015, and from the outset, the plan wasn’t to grow through scattered, smaller units; it was to consolidate. Today, our facility sits on a total land area of 25,000 sq meters. That scale allows us to describe ourselves accurately as one of India’s largest investment casting facilities at a single location, with the capability to handle large production volumes without splitting orders across multiple sites.

A single location scale isn’t just a real estate statistic. It means wax injection, shell building, pouring, heat treatment, machining, and testing all happen under one roof, under one quality system which is a meaningful advantage for OEMs who want fewer handoffs and tighter control over their supply chain.

Earning RINA Marine Approval, A Rare Distinction in India

One of our most significant recent milestones is achieving RINA marine classification approval. This matters because RINA is one of the more demanding classification societies to satisfy, and Austin Alloy Cast is only the sixth foundry group in India to receive it. More notably, we are the only pure play investment casting company in the country to hold this accreditation.

That approval sits alongside marine approvals from DNV, ABS, Lloyd’s Register, and BV giving Austin Alloy Cast a marine certification profile that few Indian foundries, and fewer still pure investment casting specialists, can match. For OEMs supplying safety critical marine and offshore programs, that’s not a marketing claim; it’s a documented, audited capability.

A Full Certification Portfolio Built Over Time

Milestones in manufacturing rarely arrive all at once they’re earned certification by certification, audit by audit. Over time, Austin Alloy Cast has built a certification portfolio that includes ISO 9001:2015 for quality management, ISO 14001:2015 for environmental management, and ISO 45001:2018 for occupational health and safety. On the regulatory side, we hold PED 2014/68/EU and UKCA approvals for pressure equipment supplied into the EU and UK, along with Indian Boiler Regulations (IBR) compliance for the domestic boiler and pressure parts market.

For OEMs in oil and gas, we also hold NORSOK M-630 Ed. 6 approval of a standard specifically relevant to materials and manufacturing procedure specifications for demanding offshore conditions. Each of these was not pursued for the sake of a longer certificate list; each one opened access to a specific class of application our customers needed us to serve.

Recognized as a Star Export House by the Government of India

Austin Alloy Cast has been certified by the Government of India as a Star Export House, a recognition tied directly to sustained export performance. Through our group’s Emporia division, which operates a dedicated overseas sales office in Singapore, we export to more than 40 countries. That combination of a domestic manufacturing base built for scale, plus a genuinely global sales and service structure is part of what the Star Export House status reflects.

Investing in Testing Infrastructure, Not Just Claiming It

A milestone we’re particularly proud of is the depth of our in-house testing infrastructure, because it’s the part of the business that directly protects every other achievement. Austin Alloy Cast runs 100% dye penetrant testing and 100% magnetic particle testing on applicable components, in-house radiography using both Ir-192 and Co-60 sources in separate dedicated facilities, and ultrasonic testing capability. Our lab includes a spectrometer covering Fe and Ni based alloys across 35 elements, validated against certified reference material samples, and dimensional inspection via CMM.

Building this in house rather than outsourcing testing to third parties was a deliberate, capital intensive decision. It’s one of the milestones that doesn’t show up as a framed certificate on a wall, but it’s arguably the one that matters most to the OEMs who depend on us.

Growing as Part of a Diversified Manufacturing Group

Austin Alloy Cast operates within a broader group that includes Metflow (steel sand castings, incorporated 2006), Galaxy Technoforge (seamless rolled rings, hot forged profile rings, bearing races, and gear blanks, incorporated 2002), and Ayushi Engineering (machined components for automotive and general engineering, established 2003). Together, this gives customers access to investment casting, sand casting, seamless rolled rings, and precision machining all from group companies operating in Western India, rather than needing to qualify separate suppliers for each process.

We’re also proud members of the EICF (Engineering Investment Casting Foundries), reflecting our ongoing participation in the industry’s standards and community, not just our own internal targets.

Investing in Sustainability as a Core Milestone

Growth at Austin Alloy Cast hasn’t come at the expense of environmental responsibility. Our facility is partially powered in part by a 1.5 MW solar power plant, a deliberate investment in green energy that supports our ISO 14001 environmental management commitments and reflects a broader group philosophy of sustainable, reliable, and affordable energy use.

What These Milestones Mean Going Forward

None of these achievements, the facility scale, the RINA and marine approvals, the certification portfolio, the Star Export House status, or the in house testing capability were pursued in isolation. Each one exists because a customer, somewhere, needed Austin Alloy Cast to prove it could meet a higher bar. That’s ultimately what milestones represent in manufacturing: not a finish line, but evidence that the next demanding program can be trusted to us.

As we continue expanding capacity and capability, our approach to reaching the next milestone stays the same as it was for the last one: invest in the infrastructure first, earn the recognition through performance, and let the certificates and approvals follow.

Why Certified Foundries Are Preferred by Global Engineering Companies

In today’s competitive manufacturing environment, global engineering companies cannot afford uncertainty in their supply chain. Whether producing equipment for power generation, mining, oil and gas, marine, transportation, or industrial processing, they depend on components that consistently meet strict quality, safety, and performance requirements. Certification is one of the main parameters influencing the choice of supplier.

Certified foundries have become the preferred choice for engineering companies worldwide because certifications provide assurance that products are manufactured under controlled processes, verified quality systems, and internationally recognized standards. Beyond compliance, certifications demonstrate a foundry’s commitment to continuous improvement, reliability, and customer satisfaction.

The Importance of Trust in Engineering Supply Chains

Engineering projects often involve significant investments, long operating lifecycles, and demanding service conditions. A single casting failure can lead to production shutdowns, costly repairs, safety incidents, or reputational damage.

For this reason, procurement teams and engineers look beyond price when selecting a casting supplier. They seek partners capable of delivering consistent quality over the long term. Certifications serve as independent validation that a foundry follows established procedures and maintains effective quality controls throughout the manufacturing process.

Customers feel more confident when they see third-party audits and accepted standards, rather than just the supplier’s word on the matter.

Consistent Quality Through Standardized Processes

One of the biggest advantages of working with a certified foundry is process consistency.

International standards such as ISO 9001 require documented procedures, quality monitoring systems, corrective action processes, and continuous improvement practices. These requirements help ensure that every stage of production is carefully managed, from raw material inspection and pattern development to melting, casting, heat treatment, machining, and final inspection.

This structured approach minimizes variations between production batches and reduces the likelihood of defects reaching customers.

For global engineering companies managing large projects, consistency is often more valuable than occasional excellence. They need confidence that the thousandth casting will perform as reliably as the first.

Improved Traceability and Documentation

Modern engineering projects demand complete traceability.

Certified foundries maintain detailed production records that allow materials, process parameters, inspections, and testing results to be tracked throughout manufacturing. This level of documentation is especially important in industries where regulatory compliance and product accountability are critical.

If a customer requires material certificates, inspection reports, heat treatment records, or mechanical testing results, a certified foundry can provide the necessary documentation quickly and accurately.

This transparency helps customers meet their own quality obligations while simplifying audits and project approvals.

Compliance with Industry Requirements

Many industries have strict standards governing the components used in critical applications.

Marine, offshore, energy, defense, and industrial processing sectors often require castings produced under recognized certification systems. Engineering companies working in these industries prefer certified suppliers because compliance requirements are already integrated into their manufacturing processes.

Specialized certifications and approvals demonstrate that a foundry has the technical capability and quality systems needed to produce castings for demanding operating environments.

This reduces qualification time and lowers the risk associated with introducing new suppliers.

Better Risk Management

Supply chain risk has become a major concern for global manufacturers.

Choosing an uncertified supplier may initially appear cost-effective, but the hidden risks can be substantial. Poor quality, inconsistent performance, inadequate documentation, delayed deliveries, and product failures can create significant financial consequences.

Certified foundries help reduce these risks through structured management systems and preventive quality controls. Problems are identified earlier, corrective actions are documented, and continuous improvement initiatives help prevent recurring issues.

As a result, engineering companies experience fewer disruptions and greater confidence in their supply chain.

Stronger Focus on Continuous Improvement

Certification is not a one-time achievement. Maintaining compliance requires regular audits, performance reviews, and ongoing improvements.

This culture of continuous improvement benefits customers directly.

Certified foundries continually evaluate production efficiency, defect rates, process capabilities, and customer feedback. Opportunities for improvement are identified and implemented systematically rather than reactively.

Over time, this leads to higher-quality castings, improved delivery performance, and more reliable manufacturing outcomes.

Global engineering companies value suppliers that actively invest in becoming better rather than simply maintaining the status quo.

Environmental and Workplace Responsibility

Many international organizations now evaluate suppliers based not only on product quality but also on environmental and workplace practices.

Certifications such as ISO 14001 for environmental management and ISO 45001 for occupational health and safety demonstrate a foundry’s commitment to responsible operations.

These standards help ensure that manufacturing activities are conducted with greater attention to environmental impact, employee safety, and regulatory compliance.

For multinational engineering companies with sustainability goals and corporate responsibility commitments, partnering with certified suppliers supports broader organizational objectives.

Supporting Global Market Expectations

Engineering companies serving international markets must meet customer expectations across multiple regions and industries. Certification provides a common language of quality that is recognized worldwide.

Whether a project is located in North America, Europe, the Middle East, or Asia-Pacific, customers often view certified foundries as lower-risk suppliers capable of meeting international requirements.

This international recognition enables the approval of suppliers and long-term business partnerships.

Why Certification Matters More Than Ever

The more demanding engineering applications and the more complex supply chains the more important supplier reliability becomes. Certifications offer tangible evidence that a foundry operates with discipline, accountability, and a commitment to quality.

For global engineering companies, the benefits are clear: consistent products, improved traceability, reduced risk, regulatory compliance, and confidence in long-term performance.

At Austin Alloy Cast, certifications are more than framed certificates on a wall. They reflect the systems, processes, and culture that support every casting we produce. By maintaining internationally recognized standards and focusing on continuous improvement, we help customers around the world secure dependable casting solutions for their most demanding engineering applications.

Common Casting Challenges Faced by Industrial Machinery Manufacturers

Cast components are the backbone of industrial machinery. Gearbox housings, pump bodies, valve assemblies, bearing blocks, and structural frames all begin as molten metal poured into a mould. When those castings are sound, the machine performs as designed. When they are not, the problems ripple outward into assembly delays, warranty claims, and equipment failures in the field.

For machinery manufacturers, understanding the challenges that lie behind casting is the first step toward avoiding them. Below are some of the most common obstacles that arise, why they happen, and what they mean for the finished product.

Porosity and Internal Voids

Few defects frustrate manufacturers more than porosity, because it often hides inside an otherwise perfect-looking part. Gas porosity forms when trapped air or dissolved gases fail to escape before the metal solidifies, leaving tiny cavities throughout the casting. Shrinkage porosity is different in origin but similar in effect. As metal cools and contracts, insufficient feeding leaves small internal holes where the liquid could not reach.

In industrial machinery, these voids are serious. A porous pump body may leak under pressure. A porous load-bearing component may fail unexpectedly under fatigue. Because the defect is internal, it frequently escapes visual inspection and only reveals itself during machining or, worse, in service. Preventing it comes down to controlled pouring temperatures, properly designed gating and risers, and clean, well-degassed metal.

Shrinkage and Dimensional Instability

All metal shrinks as it solidifies and cools, and managing that shrinkage is one of the central challenges of casting. If solidification is not controlled, the result can be sink marks, internal shrinkage cavities, or overall dimensional drift. Thick and thin sections in the same part cool at different rates, creating internal stresses that pull the component out of shape.

For machinery makers who rely on tight fits between mating parts, even small deviations matter. A housing that is a few millimeters off can throw off shaft alignment across an entire assembly. Directional solidification, thoughtful part design that avoids abrupt changes in wall thickness, and solidification modelling all help keep shrinkage predictable.

Warping and Residual Stress

Closely related to shrinkage is warping, the distortion that occurs during or after solidification as different regions cool unevenly. A component may come out of the mould looking correct, then move slowly out of tolerance as residual stresses relax over time. This is particularly troublesome for large, flat, or asymmetric parts.

Residual stress can also compromise strength, leaving a component more prone to cracking under load. Controlled cooling and appropriate heat treatment, such as stress relieving, are essential tools for keeping distortion in check and stabilizing the part before it reaches the machine shop.

Holding Tight Tolerances Consistently

Achieving a good tolerance once is not difficult. Achieving it on every part, batch after batch, is where many suppliers struggle. Machinery components often demand precision in specific areas such as bearing seats, mounting faces, and bolt patterns, where a microscopic deviation can misalign an entire system.

The challenge is that casting alone rarely delivers final machining tolerances. The realistic path is a well-produced near-net-shape casting followed by targeted precision machining on the critical features. Manufacturers who treat casting and machining as one integrated process, rather than two disconnected steps, achieve far more consistent results.

Material Selection and Metallurgical Consistency

Choosing the right alloy is a challenge in itself, since machinery components may need wear resistance, impact strength, corrosion resistance, or high-temperature performance, sometimes all at once. Getting the specification right is only half the battle. The other half is ensuring the metallurgy is consistent from heat to heat.

Variations in chemistry or microstructure can cause identical-looking parts to behave very differently under load. Metallurgical defects such as hard spots or inclusions can also ruin machinability and shorten service life. Rigorous melt control, chemical analysis, and mechanical testing are what separate dependable castings from unpredictable ones.

Surface Defects and Finish Quality

Cold shuts, misruns, inclusions, and rough surfaces all detract from both function and appearance. A cold shut, where two streams of metal fail to fuse properly, creates a weak seam. Inclusions from mould material or slag create hard points and cosmetic flaws. For components where sealing surfaces or clean finishes matter, these defects mean extra grinding, rework, or outright rejection.

Lead Times and Supply Reliability

Beyond the metallurgy, machinery manufacturers face a very practical challenge: getting quality castings on time. Long or unpredictable lead times disrupt production schedules, tie up working capital, and can stall an entire assembly line waiting on a single part. Tooling delays, capacity constraints, and quality rejections all compound the problem. A supplier who cannot deliver consistent quality on a reliable schedule becomes a liability, no matter how good the individual parts may be.

Turning Challenges into Confidence

None of these challenges are insurmountable. Porosity, shrinkage, warping, and tolerance drift are all well understood, and each has proven solutions rooted in disciplined process control, sound design, and thorough inspection. The manufacturers who succeed are those who partner with foundries that treat these issues seriously, applying experience and engineering rigour at every stage rather than reacting to defects after the fact.

Casting will always involve complexity, but with the right approach that complexity becomes manageable and the finished machinery becomes something you can build with confidence.

Why Heavy Engineering Projects Demand Custom Steel Castings, Not Standard Solutions

Heavy engineering rarely forgives compromise. Whether the project is a mining excavator, a hydroelectric turbine housing, a cement plant crusher, or a marine propulsion assembly, the components at its core operate under punishing loads, extreme temperatures, and relentless stress cycles. In this world, choosing an off-the-shelf part to save time or cost is often a decision that comes back to haunt the project. The engineers who build for the long term understand a simple truth: heavy engineering demands custom steel castings, not standard solutions.

Here is why that distinction matters so much.

Standard Parts Are Designed for Averages, Not Extremes

Off-the-shelf components exist because they serve the widest possible range of buyers. They are engineered around average conditions and generic load assumptions. That approach works well for ordinary machinery, but heavy engineering is defined by conditions that are anything but average.

A load-bearing bracket in a mining shovel, for instance, faces shock loads, abrasive dust, and constant vibration. A valve body in a power plant endures high pressure and thermal cycling for decades. Standard parts are simply not built for these specific realities. When they are forced into demanding roles, they fatigue early, crack under stress concentrations the designer never accounted for, or wear out faster than the maintenance schedule allows. The result is unplanned downtime, and in heavy industry downtime is measured in lost production worth enormous sums.

Custom Castings Match the Component to the Job

The greatest advantage of a custom steel casting is that it can be engineered for exactly one purpose. Instead of adapting a design around what already exists, engineers design the part around the actual application. That freedom shows up in several critical ways.

Material selection comes first. Different projects call for different alloys, whether the priority is high tensile strength, impact resistance, corrosion resistance, or performance at elevated temperatures. Custom casting allows the metallurgy to be tailored to the operating environment rather than accepting whatever a catalogue part happens to be made from. Steel, in particular, offers the high tensile and impact strength that load-bearing components subjected to dynamic forces genuinely require.

Geometry is the second advantage. Casting makes it possible to produce large, complex shapes as a single, structurally sound piece. Features that would otherwise require welding several parts together can be cast integrally, eliminating the weld seams that so often become points of failure. Fewer joints mean fewer weak spots, cleaner load paths, and a component that behaves as one continuous body under stress.

Complexity and Size That Fabrication Struggles to Match

Heavy engineering components are often physically enormous, sometimes weighing hundreds of kilograms or more, with internal cavities, varying wall thicknesses, and intricate contours. Machining such shapes from solid billet would waste vast amounts of material and machining time, and fabricating them from plate introduces distortion and residual stresses.

Casting sidesteps these problems. Molten steel takes the shape of the mould, so material goes only where it is needed. This conserves raw material, reduces machining, and produces near-net shapes that require far less finishing work. For large, one-of-a-kind, or low-volume components, which describes a great deal of heavy engineering work, casting is frequently the only economically sensible route.

Reliability Where Failure Is Not an Option

In sectors like mining, power generation, oil and gas, and cement production, a single failed component can halt an entire operation. The true cost of a part is never just its purchase price. It includes the risk it carries. A cheap standard part that fails in service can trigger cascading damage, safety incidents, and days or weeks of stopped production.

Custom castings reduce that risk at the source. Because they are engineered to the application, validated against the real loads, and produced with controlled metallurgy and inspection, they deliver the consistency and predictability that critical systems require. Engineers can specify mechanical properties, tolerances, and testing regimes that give them confidence the part will perform exactly as intended, batch after batch.

Precision Where It Counts

Large components still demand fine accuracy in the places that matter, such as bearing seats, mating faces, and bolt patterns. A microscopic deviation in these areas can throw off alignment across an entire assembly. Custom casting paired with precision machining allows manufacturers to hold tight tolerances precisely where the design requires them, while leaving non-critical surfaces as-cast. This targeted approach balances performance with cost far better than any standard component ever could.

Engineering for the Long Haul

Ultimately, heavy engineering is an investment measured in decades, not seasons. The machinery must run reliably long after it is commissioned, often in remote or hostile environments where replacements are difficult and expensive to install. Custom steel castings support that longevity by delivering components matched to their duty, free of unnecessary weak points, and built to endure.

Standard solutions have their place in the world of ordinary equipment. But when the stakes are high, the loads are severe, and failure is simply not acceptable, custom steel castings are not a luxury. They are the foundation on which dependable heavy engineering is built.